If you’ve ever stood on the manufacturing floor late at night, watching a CNC lathe hum through the 12th consecutive hour of work, you notice something that never makes it into product spec sheets: every curve, undercut, blind hole, and micro-notch on a precision turned part doesn’t just change its function—it changes the story of how it’s made. I’ve been a precision turned parts supplier for 18 years, and I’ve lost count of how many times a design engineer will hand over a CAD file that looks perfect on screen, only for our team to stare at it for an hour, squint at the tolerances, and wonder how we’re going to turn that ideal geometry into a part that meets their exact standards. The shape complexity of these parts isn’t just a buzzword; it’s the single biggest driver of lead times, production costs, material waste, and quality consistency on the floor. Precision Turned Parts
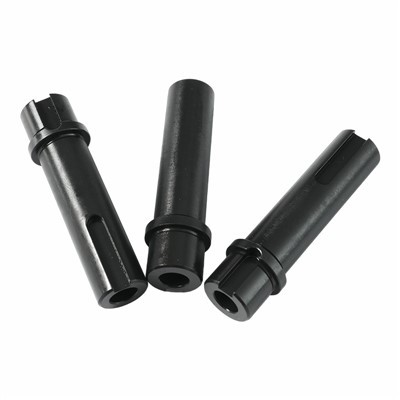
Let me start with what shape complexity actually means for turned parts, because it’s not just “more curves” or “fewer straight lines.” For a precision turned part—something made by rotating a workpiece and cutting it with a single-point tool, usually on a CNC lathe—complexity comes from features that push the limits of what a cutting tool can reach, what the machine can hold, and how the material behaves under pressure. A simple shaft with a single diameter is straightforward: load the bar stock, turn to size, part it off, done. But add a blind, threaded hole that only 1mm in diameter and 5mm deep, and suddenly you’re dealing with tool deflection (the thin drill bit bending under pressure, making the hole off-center), chip evacuation (tiny metal shavings getting stuck in the hole, causing thread stripping), and the need for a custom tool path that moves the drill in and out at specific speeds to clear debris. That’s basic complexity, but it scales fast: a part with multiple concentric undercuts, a tapered flange with a 0.002mm wall thickness, or a series of micro-notches spaced 0.5mm apart all fall into the high-complexity category.
One of the first places shape complexity hits is material waste, which is a far bigger cost than most customers expect. When you’re cutting a simple, symmetric part from a solid bar of aluminum or steel, the off-cuts are predictable—you can even re-use smaller pieces for secondary jobs. But add a complex feature like a deep, narrow internal groove, and you have to adjust your cutting strategy: slower feed rates to prevent tool breakage, which means more time spent cutting, but also a higher chance of material being scraped because of vibration or misalignment. Last year, we had a customer in the medical device sector come to us with a custom component for a surgical stapler. The original design had a series of 8 micro-undercuts along a 30mm length of 6mm diameter titanium bar. Our initial test run scraped 12% of the parts because the thin walls between the undercuts were cracking during turning—titanium is brittle, and the repeated flexing from the cutting tool would split the wall if the geometry was too sharp. We had to re-engineer the undercut radii to 0.2mm instead of the 0.1mm the engineer had designed, which reduced the complexity enough to cut scrap to 2%, but it also meant we had to adjust the overall shape, a conversation most design teams don’t realize is necessary when complexity is high. That 10% scrap difference isn’t just lost material—it’s lost machine time, lost labor, and lost opportunity to deliver parts on time.
Lead times are another casualty of shape complexity. A simple turned part can be quoted and delivered in 24 hours, from bar stock to shipping dock. A high-complexity part? We’re looking at 10 to 14 days, sometimes longer. Why? Because complexity means more steps, more setup, more testing. Let’s say you need a part with four separate internal features: two blind holes, one threaded bore, and a tapered external flange. For a simple part, you can do all of that in a single setup on a 3-axis lathe. But if the tapered flange is angled 15 degrees, the threaded bore is offset 2mm from the part’s centerline, and one blind hole only opens on that tapered face, you can’t do all that in one setup. You have to move the part to a second machine, or re-fixture it on the same lathe, which means calibrating the tooling all over again, checking alignment with a coordinate measuring machine (CMM), and running a first-article test to make sure nothing is off. Last quarter, we had an aerospace customer come to us with a fuel line component that had 11 separate features, including a spiral internal groove and a external flange with 12 evenly spaced notches. The engineer had designed it for a single 5-axis lathe, but we only had two machines capable of that kind of work, and each setup took 8 hours just to calibrate. We couldn’t take on any other jobs for two days because that one complex part tied up that equipment, pushing our lead time out for three other customers’ orders. That’s the hidden cost of complexity—its ripple effect on the whole production schedule.
Tooling and tool life are where shape complexity really starts to add up, and it’s something most customers never see on their bill, but it’s reflected in the price they pay. When you’re turning a simple part, you can use standard off-the-shelf tools—generic turning inserts, drills, taps that work for most geometries. But complex features need custom tools, or modified standard tools, to get right. A blind hole that’s deep and narrow needs a long, thin drill bit, not the standard short one that comes in a tool kit. A complex undercut needs a specially shaped turning insert, not the square one you buy for $5 a piece. Those custom tools cost 10 to 20 times more than standard ones, and they wear out faster, too. A standard drill bit might last 1,000 holes before it needs replacing, but a long, thin drill for a 1mm blind hole might only last 100. We keep a tool room with over 2,000 different inserts and custom tools, and half of them are only used for parts that have complex shapes. Last year, we had a customer in the automotive sector who switched from a simple transmission shaft to a more complex one with a series of splines along the center. Their original supplier quoted them a low price, but when they switched to us, we explained that the splines required custom hobbing tools that cost $12,000 to set up. The new supplier had used a modified standard tool, which was breaking every 20 parts, leading to downtime that ultimately cost the customer more in late fees than if they’d gone with our quoted price, even with the custom tooling. The takeaway here is that cheap tooling for complex shapes is a false economy—it leads to more downtime, more scrap, and higher overall costs in the long run.
But here’s the thing about shape complexity: it’s not always bad, and it’s not always something to be avoided. Complexity is what makes a part work the way it’s supposed to. A pacemaker’s electrical connector has micro-features that are critical to its function, even if they’re hard to machine. A jet engine fuel nozzle has internal swirl chambers that improve fuel efficiency, even if they require 5-axis turning to get right. The problem comes when complexity is added without considering manufacturability—when a design engineer specifies a geometry that works for the part’s function, but doesn’t account for what the machine, tools, and material can actually do. That’s where our job as precision turned parts suppliers comes in: we don’t just quote parts and machine them—we partner with engineers to balance function with manufacturability.
Last year, we worked with a medical device startup that was designing a new insulin pump connector. The initial design had a 0.8mm wall thickness around a threaded internal bore, with a small external notch to lock the connector into place. The engineer insisted on the 0.8mm wall because it needed to be flexible enough to bend with the pump’s plastic housing, but the notch added a stress concentration point that we knew would cause the wall to crack during turning. Instead of saying “we can’t make it,” our team took three days to run finite element analysis (FEA) simulations on the part, testing different wall thicknesses and notch shapes. We found that if we increased the wall thickness to 1.0mm and rounded the notch’s edges to 0.5mm, the part would still flex enough to work, and the cracking risk dropped from 85% to less than 1%. The customer was able to keep the function they needed, and the complexity went down enough that we cut the production time by 40% and the scrap rate to less than 0.5%. That’s the value of working with a supplier who understands how shape impacts manufacturing—we don’t just machine parts; we help make the design better.
Quality consistency is another area where shape complexity makes a huge difference, and it’s something that can have real-world consequences for the end product. When you have a part with a simple shape, it’s easy to inspect: a CMM can measure a diameter, a length, a thread pitch in a few minutes. But complex shapes have dozens of critical features, each with their own tolerances. A fuel nozzle with an internal swirl chamber might have a tolerance of 0.001mm on the chamber’s depth, a tolerance that’s impossible to measure with a standard caliper. We have a team of three dedicated quality inspectors, and half their time is spent verifying complex features on turned parts—running 3D scans, using laser micrometers, cross-referencing CAD data with actual part measurements. Last year, an aerospace customer caught a mistake from their previous supplier: a complex part with a spiral internal groove that was 0.003mm too shallow, which would have caused fuel flow issues in flight. That mistake would have been catastrophic, and it was entirely due to the supplier not taking the time to properly inspect the complex feature. At our shop, we have a rule: any part with more than three critical complex features gets a full CMM scan and a dimensional report before it leaves the floor. That adds time, but it’s non-negotiable for precision turned parts.
I talk to a lot of young design engineers who think “complex” means advanced, but what they don’t realize is that every extra feature adds a layer of risk. It’s like building a house: you can add a balcony, a basement, a curved roof, but each of those adds cost, time, and a higher chance of something going wrong. The same is true for precision turned parts. If you’re designing a part that’s going to be used in a critical application—medical, aerospace, automotive safety—you need to weigh the function you get from complex features against the cost, lead time, and risk that complexity brings. That’s why we always start a new project with a design for manufacturability (DFM) review, even if the customer doesn’t ask for it. We look at every feature, every tolerance, and ask: is this necessary? Is there a simpler way to get the same function? Can we adjust the geometry to make it easier to machine, without hurting performance?

At the end of the day, every precision turned part is a balance between what the design needs to do and what we can actually make. I’ve seen parts that were over-designed with unnecessary complexity, driving up costs and lead times for no good reason, and I’ve seen parts that were perfectly balanced, where complexity was only added where it mattered, making both the function and manufacturing work smoothly. If you’re a design engineer or a procurement manager working with precision turned parts, don’t just focus on the function or the price—pay attention to the shape. That’s where the biggest opportunities to save time, money, and reduce risk are, and that’s where the biggest mistakes can happen.
Aluminum Turned Parts If you’re working on a project with precision turned parts, whether it’s a medical device, aerospace component, automotive part, or any other application, and you’re struggling with how shape complexity is impacting your manufacturing, get in touch. We’ve been solving these problems for 18 years, and we’re here to help you find the right balance between function, cost, and delivery. Let’s talk through your CAD files, run some DFM reviews, and make sure your parts are made correctly, on time, and at a fair price.
References
- Design for Manufacturability: Reducing Costs and Improving Time-to-Market in Precision Machining. Society of Manufacturing Engineers, 2021.
- Tooling Selection and Application for Turning Complex Geometries. Machining Science and Technology, vol. 24, no. 3, 2020, pp. 412-435.
- Material Waste Reduction in Precision Turned Parts: A Study of Complex Feature Impact. Journal of Manufacturing Processes, vol. 62, 2021, pp. 789-802.
- Quality Assurance for Complex Turned Components in Critical Industries. International Journal of Precision Engineering and Manufacturing, vol. 22, no. 10, 2021, pp. 1765-1778.
Huizhou Quanyi Precision Hardware Products Co., Ltd.
Address: Building A10, 7th Floor, Zhongchuangyingke 5G Industrial Park, Zhonghan Industrial Park, Tonghu Town, Huizhou City
E-mail: info@qycncturning.com
WebSite: https://www.qycncturning.com/
